Dedicated production space for oral care compounding, filling and packing, with segregated material and finished-goods zones.
Manufacturing Facility — cGMP & FDA Registered Plant Tour
Welcome to Our State-of-the-Art Manufacturing Facility
Precision engineering meets uncompromising quality. Explore our FDA-registered, cGMP-compliant manufacturing plant designed exclusively for high-volume, premium oral care production.
HD Video
Automated Tube Filling Loop
25,000 m²
Dedicated Production Space
96M
Units Produced Annually
Guangdong
Near Shenzhen & Guangzhou Ports
Facility Capabilities at a Glance
Built for Industrial Scale and Unmatched Purity
A quick, hard-hitting summary of the physical plant’s specifications, assembled to satisfy B2B procurement checklists before the first call.
Installed capacity exceeding 96 million finished units per year across 10 automated production lines.
Class 100,000 (ISO 8) automated compounding and filling zones with HEPA filtration and controlled pressure cascades.
Pharmaceutical-grade electrodeionization and reverse osmosis water systems — the foundation of every premium toothpaste batch.
The Production Workflow
Zoned Production for Zero Cross-Contamination
A walkthrough of the physical plant layout, demonstrating strict adherence to unidirectional flow and cGMP material handling from dock to dispatch.
Zone 01

Raw Material Quarantine & Storage
Climate-controlled warehousing where all inbound active ingredients, abrasives and flavors are held under quarantine status until released by the laboratory. Every lot is barcoded on receipt and cannot reach the compounding floor without a documented release.
Zone 02

Automated Compounding Stations
High-shear, 316L stainless steel vacuum homogenizers ranging from 500L to 5,000L. Engineered for de-aeration to ensure bubble-free, perfectly smooth paste rheology before the batch is transferred to the filling hall.
Zone 03

High-Speed Tube Filling Lines
Multi-lane filling suites utilizing ultrasonic and hot-jaw sealing technology. Capable of handling ABL, PBL and aluminum tubes with precision weight controls and inline rejection of out-of-tolerance fills.
Zone 04

Secondary Packaging & Palletizing
Automated carton formers, leaflet inserters and shrink-wrapping, followed by robotic palletizing, so finished goods leave the line ready for distribution-center receipt and export consolidation.
In-House Laboratories
In-House R&D and Quality Control Laboratories
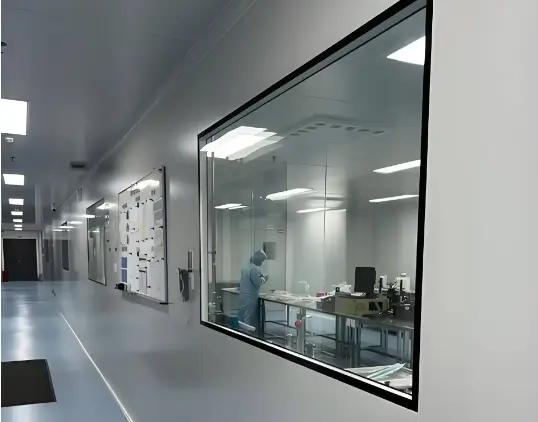
Testing happens on-site, not only through third parties. Because oral care is a mucosal-contact product, keeping assay, microbiology and physical testing inside the plant shortens release times and keeps every result traceable to the batch it belongs to. See how our QA/QC team enforces it.
Microbiology Lab
Segregated clean space for pathogen screening (USP <61> and <62>), Preservative Efficacy Testing (PET), and routine environmental monitoring of the factory floor, water loops and compressed air points.
Physical Testing Lab
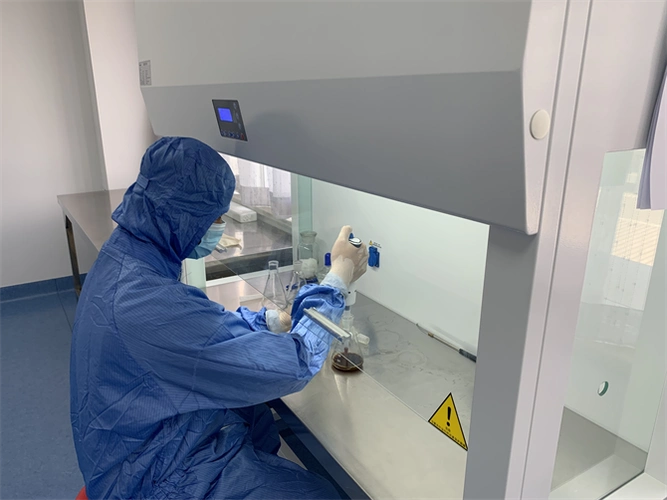
Real-time monitoring of pH, viscosity, specific gravity and tube seal burst-pressure limits, so rheology drift or a weak crimp is caught on the shift it happens rather than at final release.
Analytical Chemistry Lab
Equipped with HPLC and GC-MS instrumentation to assay fluoride levels, verify active ingredient dispersion and conduct heavy metals screening against the limits of your destination market.
Smart Manufacturing
Smart Manufacturing & Batch Traceability
Industry 4.0 capabilities that give enterprise buyers a defensible audit trail. If a question is ever raised about a lot, the answer should be a query, not an investigation.
ERP Integration
End-to-end digital tracking from the moment raw materials enter the dock to the final shipped pallet, linking each finished carton back to its ingredient lots and line parameters.
Automated Dosing
PLC-controlled raw material weighing eliminates human error in highly sensitive active-ingredient ratios, with deviation alarms that stop the batch instead of flagging it afterwards.
Inline Vision Systems
High-speed optical cameras check every tube for correct lot code printing, seal integrity and label alignment before cartoning, rejecting non-conforming units automatically.
Sustainability
Engineered for Sustainable Production
Environmental performance is now a scored line item in most enterprise supplier assessments. These initiatives are built into the plant itself rather than added as reporting afterthoughts. Read more about our sustainability programme.
- Energy-efficient HVAC and HEPA filtration systems with ambient heat recovery, cutting the load of continuous cleanroom air changes.
- Closed-loop water cooling systems for the compounding jackets, minimizing water waste across long heating and cooling cycles.
- Zero-landfill and strict recycling protocols for laminate tube scrap and cardboard waste, with segregated collection at every production zone.
Compliance
Always Audit-Ready
The regulatory backbone of the physical plant is maintained continuously, so an inspection is a demonstration of normal operations rather than a special project. Watch the plant on video before scheduling a visit.
- FDA registered facility, open to unannounced inspections.
- ISO 22716 certified for Cosmetics Good Manufacturing Practices.
- On-site quality assurance managers overseeing all line clearances and sanitization protocols.
- Welcome policy for client-led or third-party physical factory audits, including Intertek and SGS.
Factory FAQs
Facility Frequently Asked Questions
The questions supply chain and compliance teams ask us most often before a first audit.
The plant is in Baiyun District, Guangzhou, Guangdong, in the Pearl River Delta — one of the world’s densest manufacturing and export corridors. That location puts us within a short trucking radius of the Shenzhen and Guangzhou ports, plus Nansha and Shekou terminals, which shortens inland haulage, simplifies export consolidation and gives you a wide choice of carriers and sailing schedules. Our sales and project office is in Guangzhou.
Yes, and we encourage it. Client-led audits and third-party audits (Intertek, SGS, Bureau Veritas and others) are welcome at any stage, including before a Master Services Agreement is signed. If travel is not practical, we run live virtual tours over video that walk the compounding hall, filling lines, laboratories and warehouses in real time, with documents shared on screen as we go. Tell us the standard you audit against and we will have the relevant records pulled in advance.
Where a project needs it, yes. Dedicated or campaign-dedicated lines can be scheduled for allergen-free, halal, vegan, sensitive-care or pediatric runs so the equipment is not shared with conflicting formulations in the same production window. We confirm the zoning and scheduling approach with you during project scoping, because the right answer depends on your volumes, your claim set and how frequently you intend to reorder.
Changeovers such as mint to fruit follow a documented cleaning validation protocol: strip-down, Clean-In-Place cycles on the compounding vessels and transfer lines, verified rinse sampling, and a signed line clearance by a QA manager before the next batch is charged. Flavor carry-over limits are set per product family, and swab or rinse results are retained in the batch record, so you can request the evidence for any changeover in your production history.
Final Step
See Our Production Lines in Action
Tell us what you need to verify and we will open the plant to you — on screen or in person. No staged footage, no representative photos: the lines you see are the lines that would run your product.
- Live virtual tours scheduled within two business days.
- Plant capability deck and spec sheet sent with your booking confirmation.
- Quality and production managers join the call, not only sales.
Message us on WhatsApp with your product type, target volume and destination market — we reply within one business day.